

A used vertical machining center can be the best money a shop spends, or a year of chasing alarms. The difference is rarely the brand or the year. It is the hours, the spindle, the tool changer, the options that are actually turned on, and what it takes to get the machine running on your floor.
We buy and sell VMCs every week out of a 225,000 sq ft showroom and ship nationwide. This guide walks through what we check, in order, using machines that are in our used vertical machining center inventory right now.
1. Size the machine to the work, not the ad
Start with your biggest part and your hardest material. That sets the travels, the table load, and the spindle taper. Then look at machines.
- 30 taper is built for speed on small aluminum and steel parts, drilling and tapping. Light cuts, fast tool changes.
- 40 taper is the general job-shop machine. Most shops live here.
- 50 taper is for heavy cuts, big face mills, and steel and iron all day. Bigger footprint, bigger rigging bill.
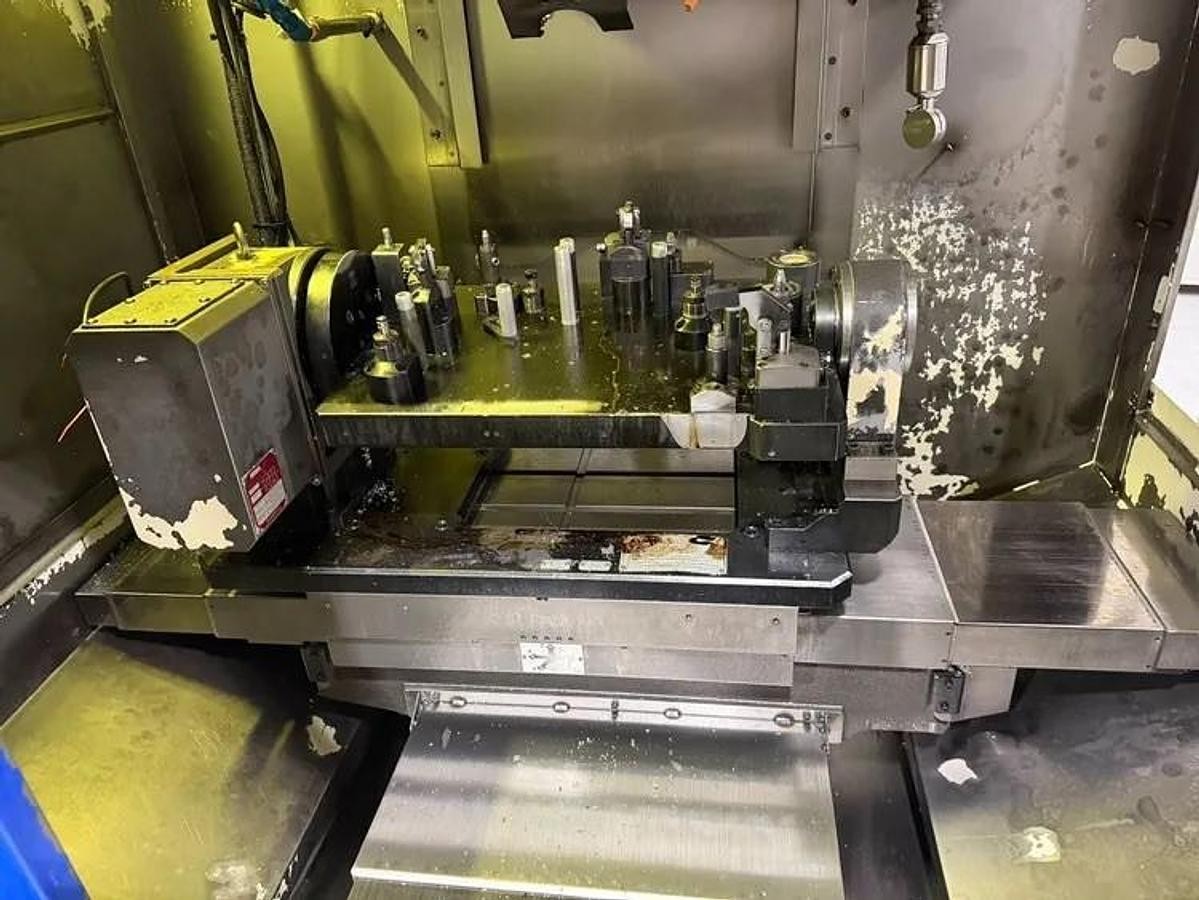
Three examples on the floor this week show the spread. The 2015 Brother Speedio S500X1 is a BT30 machine with a 10,000 RPM spindle, 19.7 in of X travel, and a 21-tool magazine. The 2022 Haas VF-2 is CAT40 with 30 x 16 x 20 in travels and a 36 x 14 in table. The 2022 DN Solutions MYNX 6500/50 II is CAT50 with a 6,000 RPM spindle, 50 in of X travel, and a 2,205 lb table load.
2. Read the hours off the control
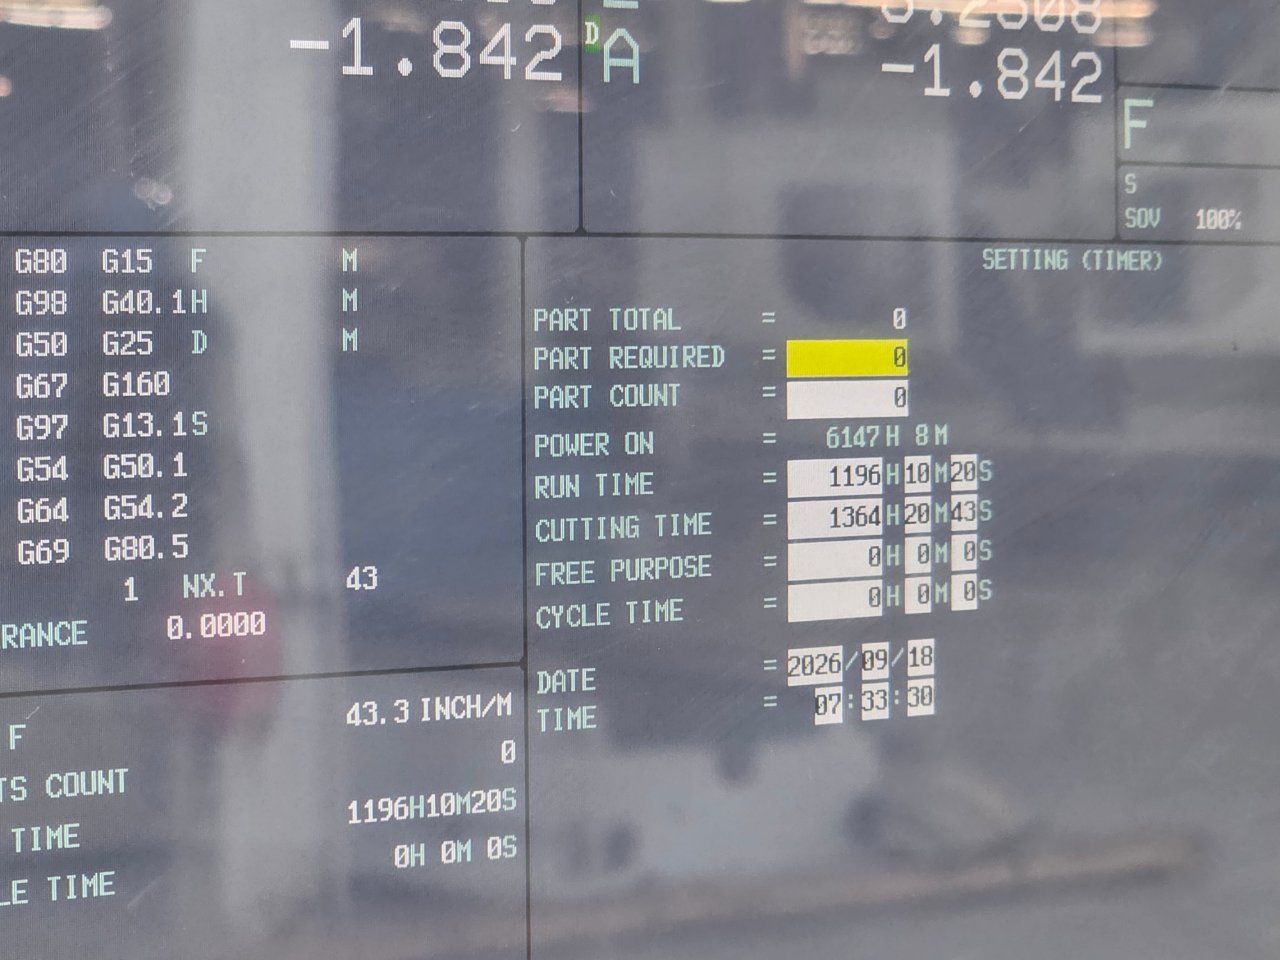
A VMC listing that says “low hours” means nothing without a photo of the timers. Most controls track several clocks. Power-on time is how long the machine sat with the lights on. Cycle or run time is how long it ran a program. Cutting time is how long it was actually feeding. Spindle and way wear follow the last two, not the first.
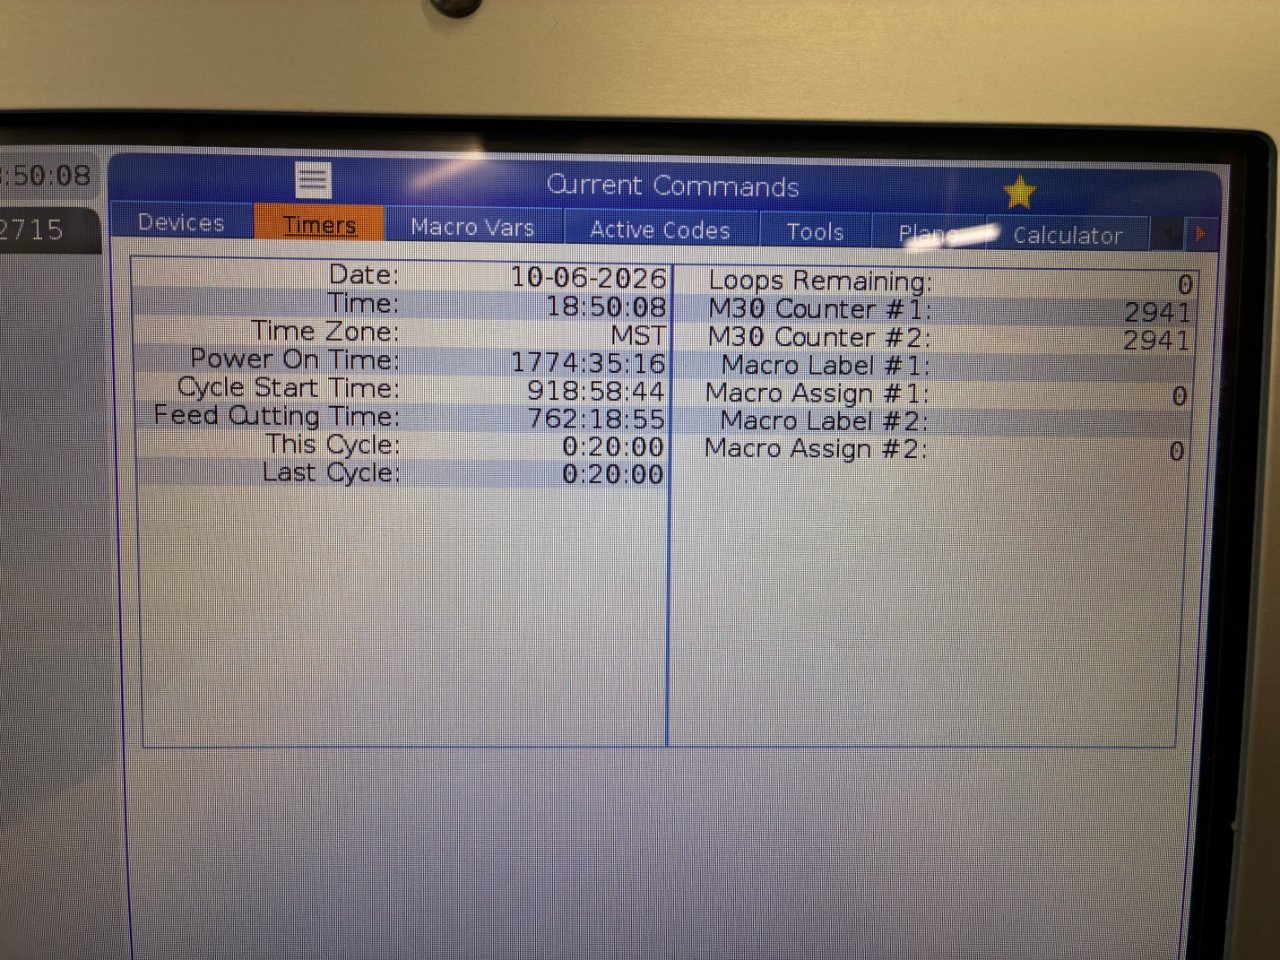
The gap between those clocks matters. Our Sharp SV-4020 lists 20,465 power-on hours but only 472 cutting hours. Most of its powered-up time was not spent cutting, and that is a very different machine from one with 20,000 hours in the cut.
3. Run the spindle through its range
The spindle is the most expensive single repair on a VMC. Have the seller run it from low RPM up to max and back, then hold it at the top for a few minutes. Listen for bearing noise and watch for heat or vibration. Put an indicator on a test bar for runout. Check that the drawbar clamps and releases a tool cleanly, and if the machine has through-spindle coolant, run it.
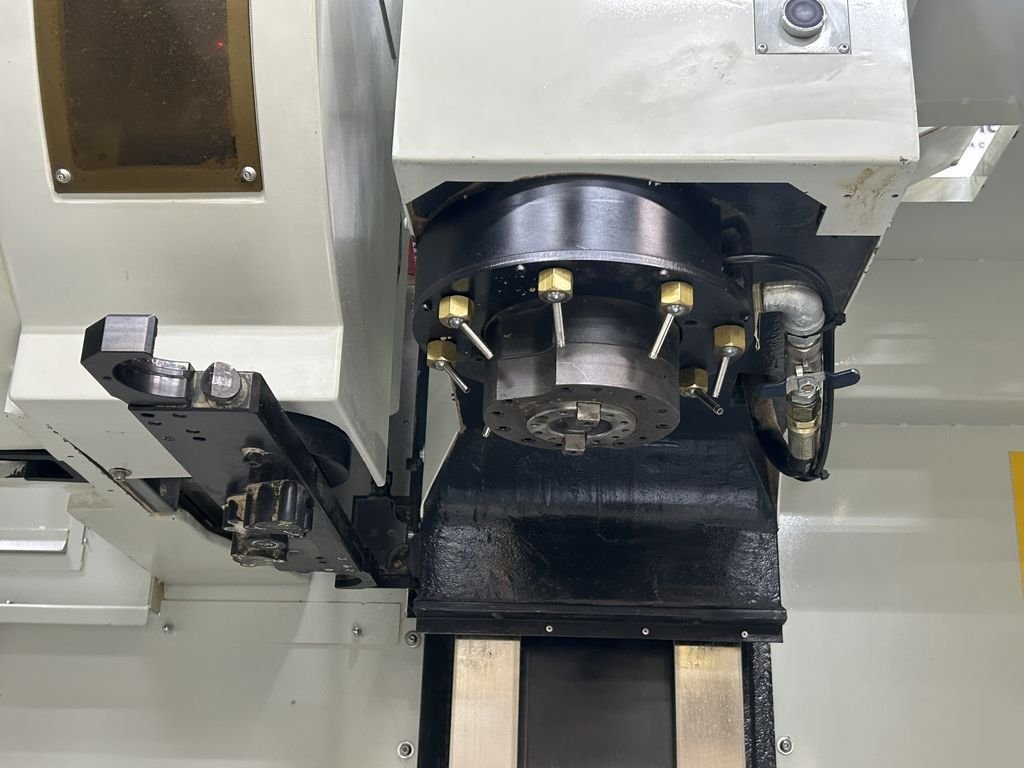
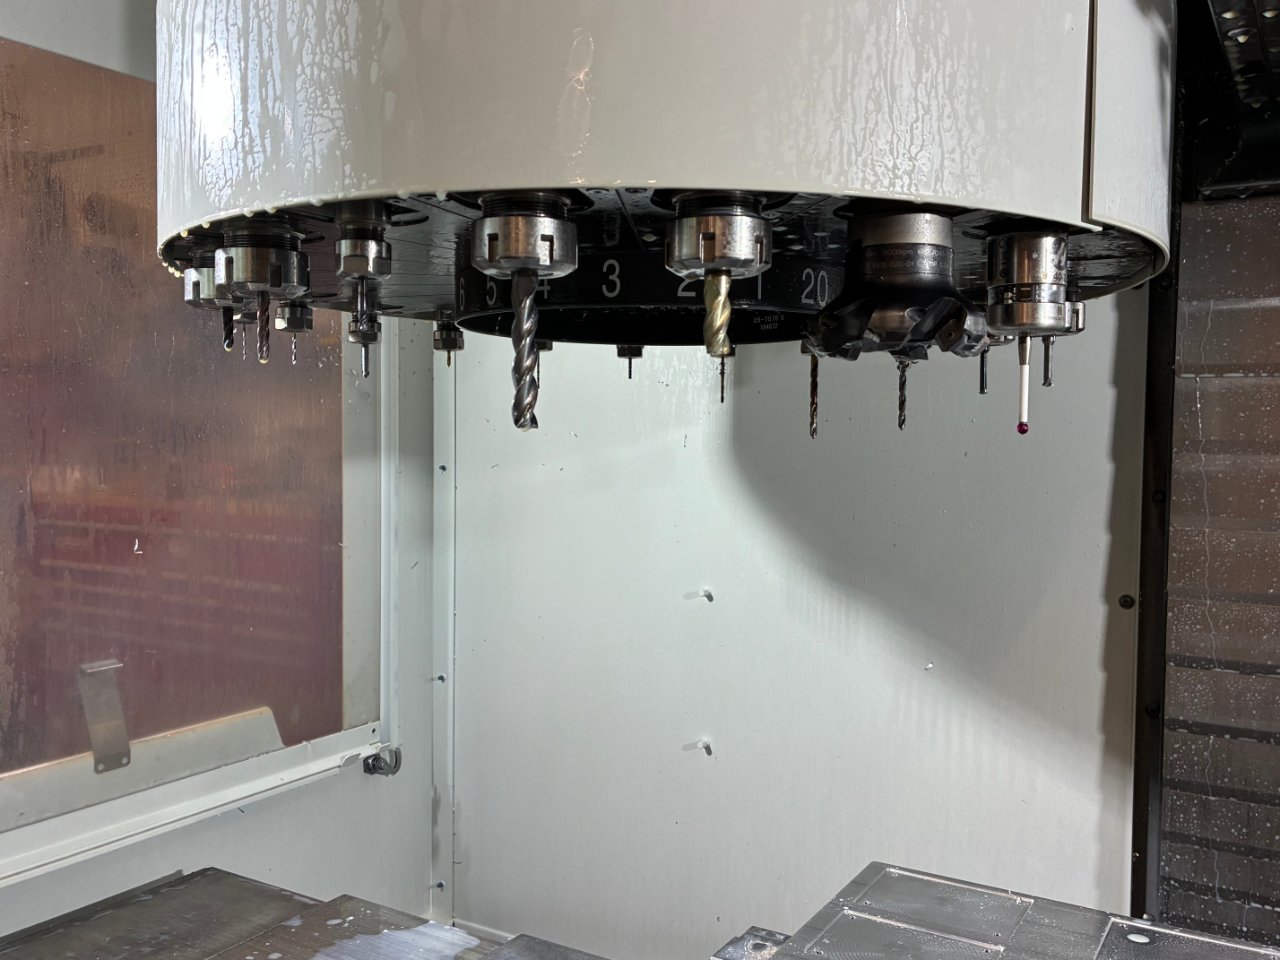
4. Cycle every pocket in the tool changer
Tool changers fail in boring ways: a pocket that will not index, an arm that drops a tool, a magazine that loses count. Call every pocket, not just the three tools in the program. Watch the change at full speed and listen for banging.
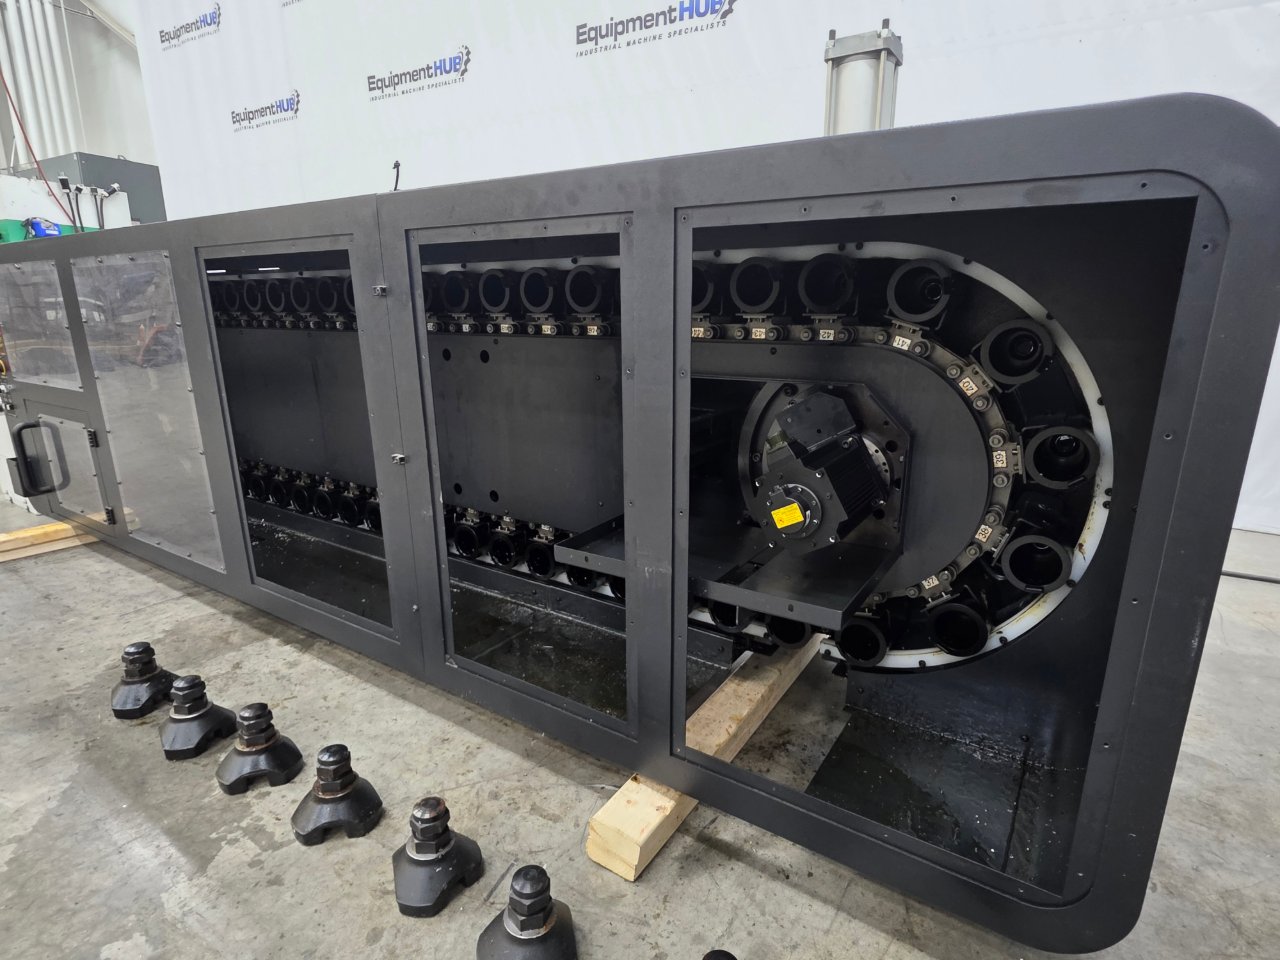
Bigger machines often ship with the magazine taken off. That is normal, but it is not free. Budget for reassembly, alignment, and a tech visit.
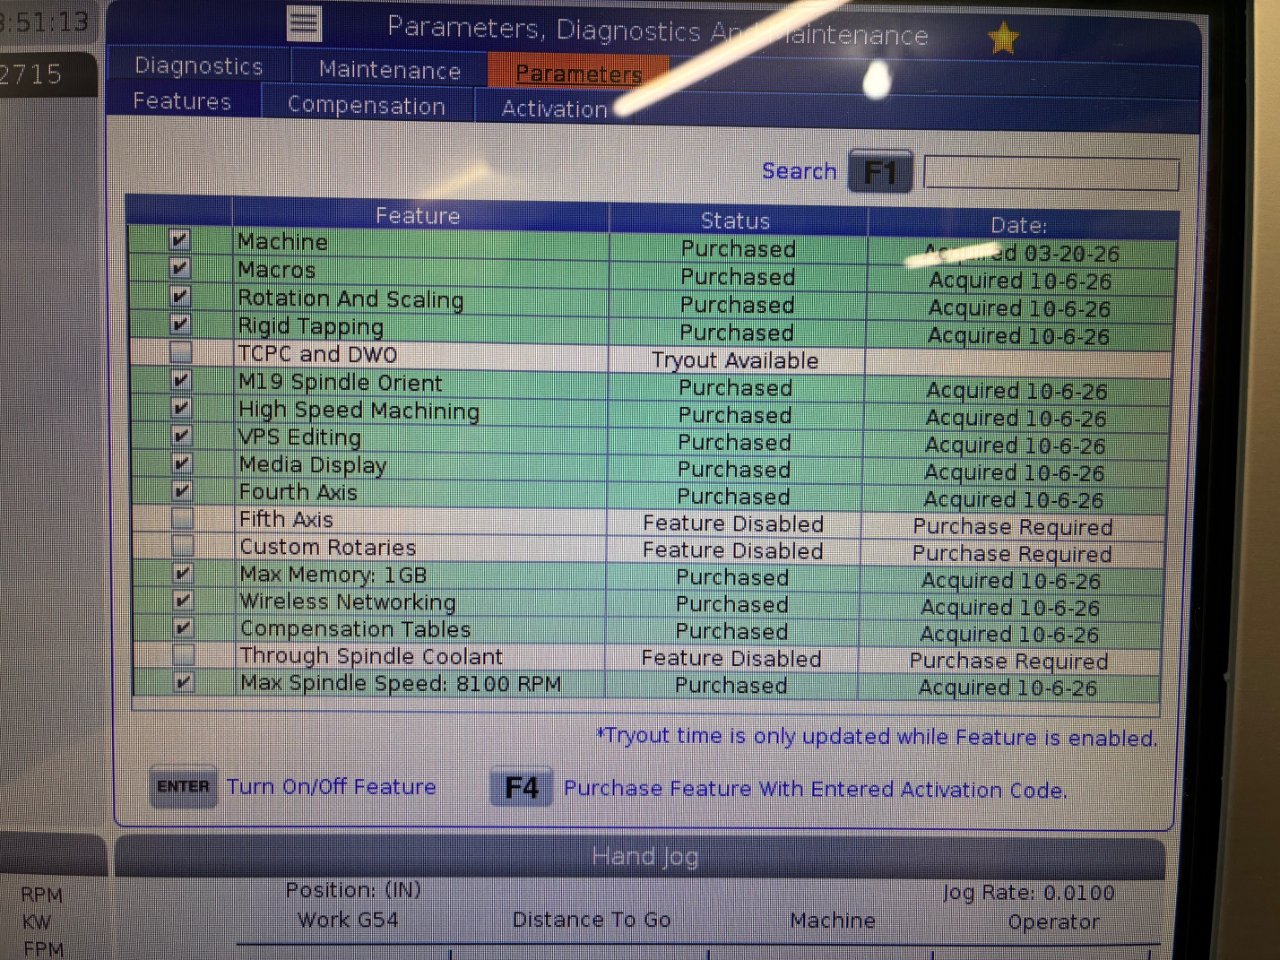
5. Check what options are actually turned on
This is where buyers get surprised. Options on modern controls are software. A machine can have the hardware and still not have the feature active. “Ready” in a listing means the plumbing or wiring is there. It does not mean the feature is paid for.
6. Ways, table, power, and the move
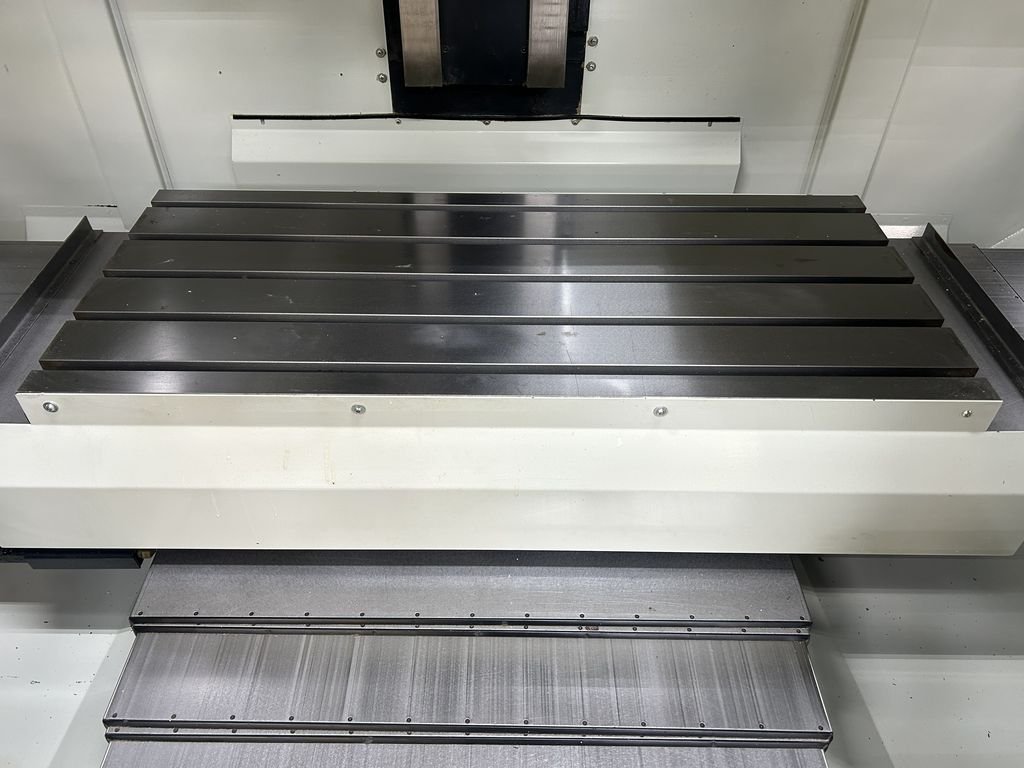
- Table and ways. Look for dings, low spots, and a worn patch where every job sat. Pull back the way covers if you can. Indicate each axis for backlash.
- Coolant and lube. A clean coolant tank and a working lube system say a lot about how a machine was kept.
- Power. Confirm voltage before you buy. The Haas VF-2 lists 460V 3-phase. The Sharp SV-4020 and the DN Solutions list 220V 3-phase. A transformer is real money.
- Weight and rigging. The Haas lists about 9,000 lbs, the Sharp about 16,000 lbs, and the DN Solutions about 20,944 lbs. Plan the truck, the rigger, the door, and the floor.
The shot list to ask for
Before you send a deposit on a used VMC, get these photos or a live video:
- Full front view under power, doors open, with the control on.
- The timers screen: power-on, run or cycle time, and cutting time.
- The options or features screen.
- The spindle running up to max RPM, and the spindle nose up close.
- The tool changer cycling through every pocket.
- The full table, the way covers, and the coolant tank.
- The data plate and the electrical cabinet.
Want the general version for any CNC? See what to inspect before you buy a used CNC machine, and the money side in used vs new CNC.
Sell us your VMC, or shop what is live
Have a vertical machining center you no longer need? Start at sell machinery. Send make, model, year, travels, taper, control, hours from the timer screen, and whether it runs under power. We buy outright and consign, and we explain both in dealer buy vs consignment. Shopping instead? Browse used vertical machining centers and the full used machinery inventory. Stock turns fast. If you do not see the size you need, ask and we will look.
Sign Up for Our Newsletter
Sign up for our newsletter using the form below to get company insights and updates directly in your inbox!